Q Construction Lifters on a Hemi: MDS vs Non-MDS Specs
The notorious “Hemi tick” often traces back to failed roller lifters eating directly into the camshaft. In Gen III Hemi engines, Q construction lifters designate hydraulic roller units engineered with reinforced roller axles, precision-metered oil passages, and heavy-duty internal valving designed to maintain consistent hydraulic lash under demanding operating conditions.
Understanding how these lifters function helps owners differentiate between failure-prone factory hardware and high-durability performance alternatives. The following breakdown covers internal lifter mechanics, common wear patterns, diagnostic methods, and the precise installation parameters required to keep your valvetrain reliable.
Prime for Young Adults — 6 Months Free
Students and 18–24s get six months of Prime free, then half price.
Start 6 Months Free
Q Construction Lifters on a Hemi: Design and Function Overview
Recommended Best Deal Products


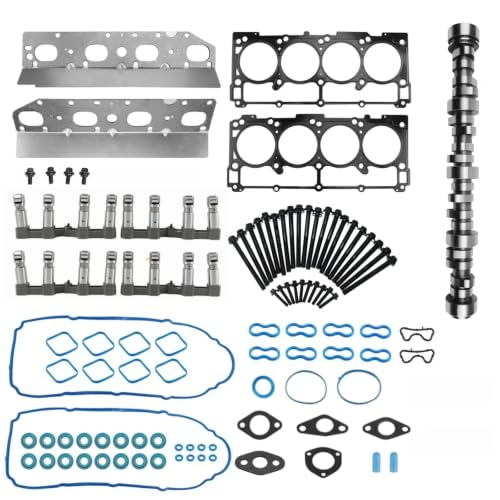
Gen III Hemi engines utilize hydraulic roller lifters positioned inside the engine block’s lifter bores. These components translate camshaft lobe lift into vertical motion, driving pushrods and rocker arms while managing high mechanical loads within modern cylinder heads.
What Defines Quality Construction in a Hemi Hydraulic Lifter
The standard Gen III Hemi lifter body features an outside diameter (OD) of 0.842 inches, matching the historic Chrysler and GM small block lifter bore standard. Quality construction depends directly on the machining accuracy of this 0.842-inch outer shell to ensure consistent oil pressure feeds to the internals.
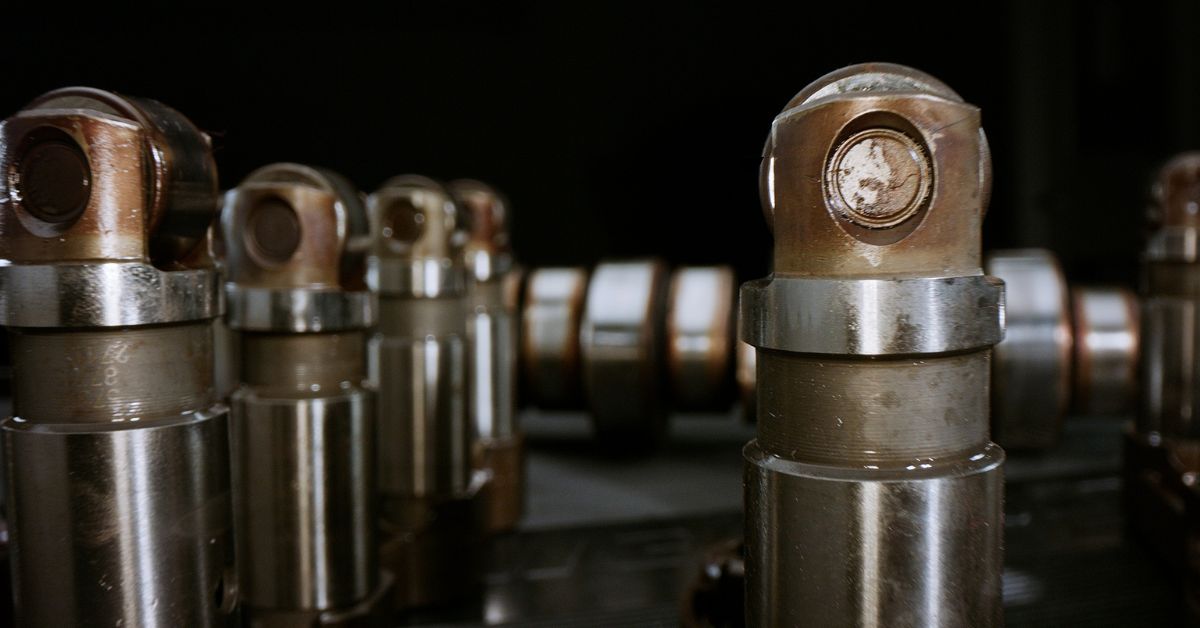
For example, while production factory lifter bodies accommodate standard manufacturing variances of up to ±0.0005 inches, performance-oriented precision-ground lifter bodies maintain strict tolerances within ±0.0001 inches. This tighter clearance prevents excessive oil bleed-by between the lifter body and the block bore.
Inside the body, quality builds rely on a rigid plunger mechanism and internal check valve. This hydraulic assembly self-adjusts using engine oil pressure, maintaining zero valvetrain lash across all operating temperature cycles as the aluminum cylinder heads and steel valvetrain expand and contract.
Role of the Roller Wheel and Needle Bearing Assembly
At the base of the lifter, a roller wheel makes direct contact with the camshaft lobe. This interface significantly reduces friction compared to older flat-tappet systems, allowing the engine to support steeper lobe profiles and higher engine speeds without excessive heat generation.
Quality construction relies on precision needle bearings packed tightly inside the roller wheel, spinning around a case-hardened roller axle. This reinforced assembly distributes load evenly, enabling the lifter to withstand aggressive camshaft ramp rates and high seat pressures without deflecting under rapid valve acceleration.
Internal Engineering Details of Gen III Hemi Lifter Construction
The internal architecture of Gen III Hemi lifters functions as a dynamic hydraulic cushion. It continuously balances oil feed against spring pressure to neutralize valvetrain lash across all engine operating temperatures.
Plunger Cavity, Return Spring, and Metering Valve
Inside the lifter body, a precision-ground steel plunger rests on a heavy-duty return spring. A cross-sectional view of oil flowing past the check ball into the high-pressure lower plunger chamber illustrates how lash take-up occurs whenever the lifter base rides the camshaft base circle.
Audible — Listen Free for 30 Days
One free credit a month and thousands of titles included.
Listen Free for 30 DaysEngine oil operating pressure runs between 30 to 65 psi, varying by engine RPM, operating temperature, and oil viscosity. This delivery pressure unseats the internal check ball, filling the reservoir before the cam lobe begins its upward ramp.
As the cam lobe lifts, pressure spikes shut the check valve instantly. The internal plunger and metering valve regulate the leak-down rate to stabilize valve events at high RPM, preventing lifter collapse under heavy valve spring resistance.
Needle bearings inside the roller wheel endure high spring loads, making oil film strength critical. If engine oil thins or pressure drops below operational thresholds, boundary lubrication fails, accelerating roller pin friction.
Pushrod Seat and Rocker Oil Metering
At the top of the plunger assembly sits the pushrod seat, engineered with an integrated metering orifice. The pushrod seat supplies pressurized oil up through hollow pushrods to the rocker assemblies, delivering continuous lubrication to the rocker trunnions, pushrod tips, and valve stems.
This controlled oil path restricts excessive top-end bleed-off. Maintaining consistent fluid volume within the lifter core dampens valvetrain shock and prevents oil aeration during aggressive valve seating events.
MDS vs Non-MDS Q Construction Lifters on a Hemi Engine
Recommended Best Deal Products


The Gen III Hemi architecture relies on two distinct hydraulic roller lifter designs across its displacement range. Choosing between Multi-Displacement System (MDS) lifters and solid-body non-MDS lifters determines your valvetrain’s operational ceiling, structural integrity, and longevity under aggressive camshaft profiles.
How MDS Deactivation Locking Pins Function
MDS lifters are installed exclusively in cylinders 1, 4, 6, and 7 on MDS-equipped 5.7L and 6.4L engines. These assemblies use spring-loaded internal locking pins and a collapsible outer sleeve designed to disengage valve motion when commanded by the powertrain control module (PCM).
When the PCM signals cylinder deactivation, solenoids vent oil pressure away from the lifter body. This pressure drop retracts the locking pins, allowing the outer body to compress without transferring camshaft lift to the pushrod.
Audible Premium Plus — Annual Membership
12 audiobook credits up front, plus the full Audible catalogue.
See Annual PlansThis mechanical complexity increases failure rates on cylinders 1, 4, 6, and 7 compared to standard cylinders 2, 3, 5, and 8. The constant cycling, oil dependency, and pin shear stress make deactivation lifters far more prone to sticking and premature collapse.
Structural Advantages of Non-MDS Hellcat and SRT Lifters
Non-MDS lifters, including Hellcat and SRT variants, feature a continuous, one-piece cold-forged body. Because they eliminate internal bypass locking pins and separate outer sleeves, they provide maximum structural rigidity across high-lift cam profiles and elevated cylinder pressures.
Solid-body lifters maintain full hydraulic integrity under heavy spring pressures and forced induction. Converting from factory MDS to non-MDS lifters requires installing a non-MDS camshaft with uniform lobe geometry and electronically disabling MDS solenoid control within the PCM software.
How to Read This Lifter Comparison Table
This table compares the physical and mechanical boundaries separating factory Gen III Hemi MDS lifters from non-MDS and SRT-grade units. Lifter Body Construction identifies whether the component relies on an outer sliding sleeve assembly or a rigid, continuous shell.
High-Spring Pressure Tolerance reflects the component’s ability to resist physical deflection under aftermarket open spring loads exceeding standard ratings. Camshaft and PCM parameters indicate the necessary companion hardware changes during an upgrade.
Values represent genuine production architecture traits across 5.7L, 6.1L, 6.2L, and 6.4L Gen III variants. When performing an MDS delete, verify exact camshaft core requirements and tuning definitions with your tuner, as software switches vary across engine control unit years.
Critical Facts Behind Hemi Lifter Failure and Roller Axle Wear
Gen III Hemi lifter failure is primarily caused by needle bearing failure in the roller wheel, causing the roller to lock up and grind down the camshaft lobe. This mechanical breakdown stems from hydraulic oil flow dynamics, heat concentration, and severe friction at the roller-to-lobe contact surface.
Low-RPM Oil Starvation and Needle Bearing Seizure
Extended engine idling reduces splash lubrication to the lifter valley, contributing to needle bearing micro-pitting and heat buildup. The roller wheel bearings rely on pressurized feed through the lifter body and supplementary oil mist thrown from the rotating assembly.
At idle speeds between 500 and 700 RPM, oil pump output drops to minimum operational thresholds. This reduction limits the volume of oil reaching the lifter trunnion, leaving the miniature needle bearings operating in a boundary lubrication state.
Without adequate oil film thickness, high frictional heat causes microscopic surface fatigue and micro-pitting on the needle pins. The damaged needles eventually skew within the bearing race, wedging together and seizing the roller axle firmly in place.
The Mechanics of Camshaft Lobe Wiping and Metal Debris Contamination
Seized needle bearings lock the roller wheel, causing it to slide rather than roll across the camshaft lobe. Instead of rolling smoothly over the profile, the stationary roller face behaves like a fixed scraper against the rotating camshaft surface.
This sliding friction generates extreme localized wear in a short operational window. In severe cases, a seized roller wearing a 0.125-inch groove into a 5.7L camshaft intake lobe can completely eliminate valve lift and cause severe misfires.
Metal debris from a failed lifter roller spreads through the engine oil passages, requiring a thorough oil system flush and often oil pump replacement. Dispersed needle bearing debris contaminates oil galleries, scoring the oil pump relief valve and threatening rod bearings.
Failing to replace a wiped camshaft when installing new lifters guarantees rapid destruction of the new components. The sharp, grooved edges of the damaged cam lobe act like a cutting tool, destroying a replacement roller wheel within minutes of initial startup.
Ticking Diagnosis Info: Lifter Roller Failure vs Exhaust Leak
Recommended Best Deal Products
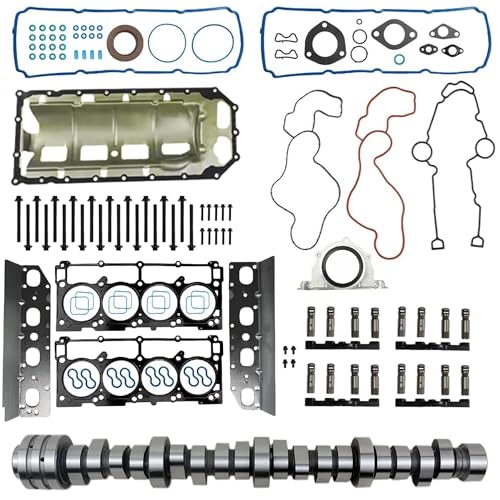


A mechanical lifter failure produces a distinct metallic tapping sound often confused with the common cracked exhaust manifold or broken manifold bolt tick. Differentiating between these two issues prevents costly, unnecessary engine teardowns.
Acoustic Differences: Cold Start Tick vs Constant Metallic Rapping
Broken rear manifold bolts (cylinders 7 and 8) produce a rhythmic ticking that mimics collapsed lifters but fades as metal expands under heat. During a cold start, escaping exhaust gas creates a sharp pop that subsides within minutes once thermal expansion seals the flange gap.
In contrast, a mechanical lifter tick remains constant or grows louder as oil heats up and drops in viscosity. As hot engine oil thins, internal hydraulic pressure bleeds down faster, exacerbating clearance lash and generating an unrelenting metallic rap at camshaft speed.
Inspecting Manifold Studs Before Tearing Down the Top End
Using a mechanical stethoscope on the cylinder head vs. inspecting manifold heat shields avoids unnecessary engine teardowns. Follow this diagnostic sequence to pinpoint the noise source:
Inspect the rear exhaust studs near cylinders 7 and 8. Feel behind the factory heat shields for broken bolt heads, loose studs, or powdery black carbon tracking along the exhaust ports.
Place a mechanic’s stethoscope directly on the valve cover near the oil fill neck versus probing the rear exhaust header flange. Valvetrain clatter resonates crisply through the valve cover, whereas exhaust ticks peak at the flange.
Idle the engine until coolant reaches 200°F. If the noise disappears entirely, suspect an exhaust leak. If the ticking persists or intensifies when oil pressure stabilizes, internal lifter failure is confirmed.
Upgrading to Premium Q Construction Lifters on a Hemi Build
OEM Hellcat Non-MDS Lifters vs Johnson Lifters
OEM Hellcat non-MDS lifters provide a cost-effective upgrade path for mild-to-moderate Gen III Hemi builds. Engineered with heavy-duty roller pins and fortified axles, they deliver significantly higher load capacity than standard production lifters while maintaining full compatibility with factory oil galleys.
For high-performance competition applications, aftermarket Johnson 2110R and short-travel lifters offer superior hydraulic control. These premium units feature slow leak-down rates and precision valving that prevent internal plunger collapse against high seat-pressure valve springs.
Plunger travel directly influences valvetrain stability at elevated engine speeds. For example, comparing standard 0.120-inch plunger travel to Johnson short-travel 0.058-inch total travel reveals that shorter internal movement virtually eliminates hydraulic pump-up and valve float under 6,800 RPM loads.
How to Read Technical Lifter Specifications
The technical parameters in this table define the operating thresholds of upgraded lifter assemblies. Total Plunger Travel indicates internal piston stroke in decimal inches (in); lower values act closer to a solid lifter to preserve duration under extreme spring forces.
Axle Pin Reinforcement denotes metallurgical toughness where the roller wheel interfaces with the lifter body. Recommended Maximum RPM (RPM) indicates safe sustained engine speeds before dynamic instability occurs. Note that exact RPM ceilings vary depending on pushrod wall thickness, spring open pressures, and lobe acceleration rates.
Plastic Yoke Trays vs Aftermarket Tie-Bar Systems
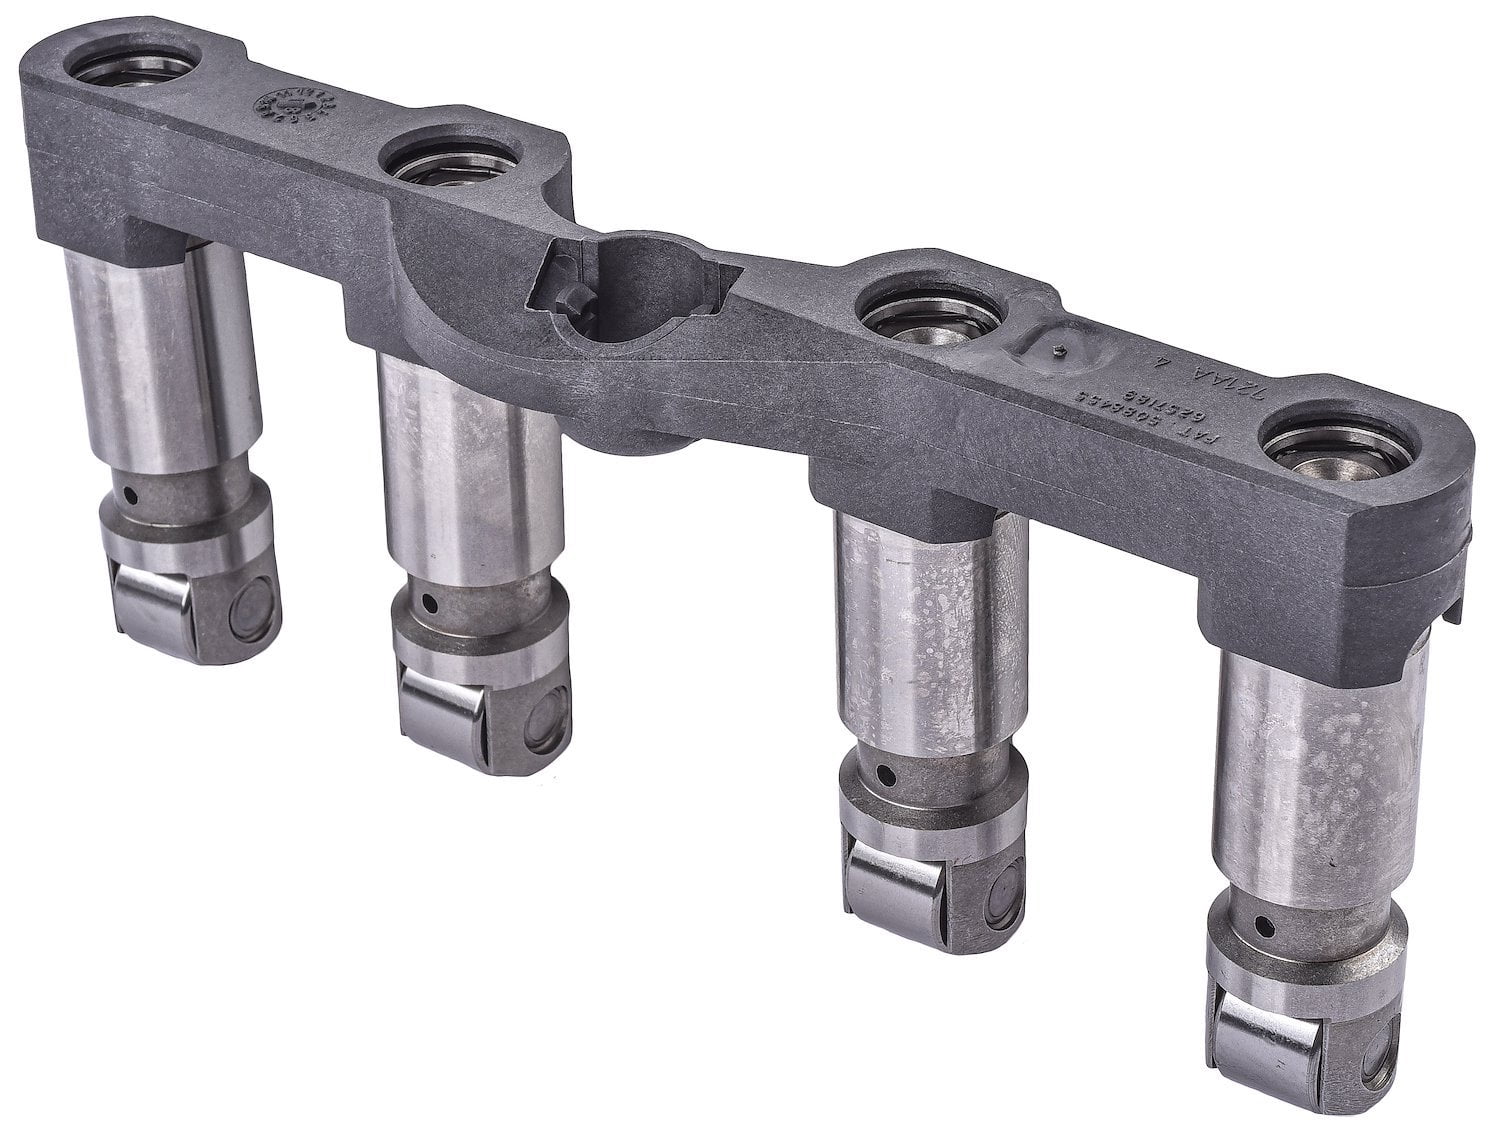
Factory Gen III Hemi setups use molded guide trays to keep roller wheels parallel to camshaft lobes. Lifter guide trays are made of plastic and wear over time due to heat cycling and high spring loads.
Reusing worn trays can allow the new lifter to twist and immediately wipe the camshaft during initial break-in. Once a lifter rotates out of alignment, the flat edge of the roller digs into the cam core.
Link-bar and tie-bar lifters eliminate reliance on factory plastic guide trays entirely. These assemblies connect paired lifter bodies with a mechanical steel link-bar, preventing lifter body rotation in aggressive performance applications where high lift and extreme RPM cause plastic deflection.
Installation Guide: Lifter Preload and Yoke Alignment on a Hemi
Replacing Plastic Lifter Guide Trays
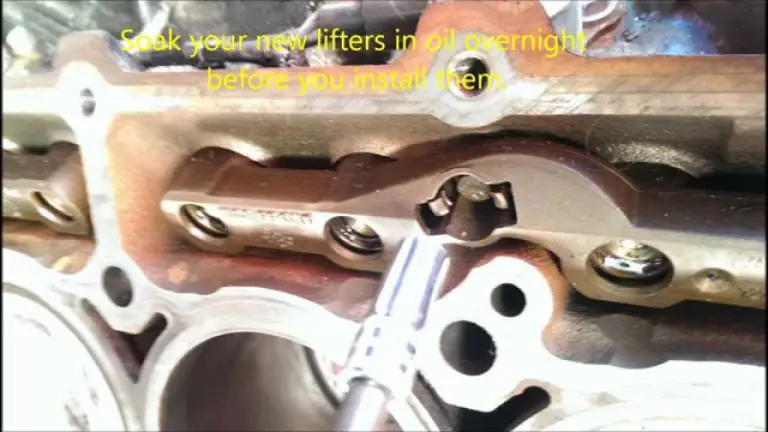
Submerging lifters in clean engine oil prior to installation ensures the internal check valve and reservoir purge trapped air. Liberally coat the exterior roller wheels and internal needle bearings with a high-pressure assembly lube to eliminate dry friction during initial startup cranking.
Never reuse plastic alignment trays. While the plastic yokes may look intact upon removal, their internal flats stretch and wear down from continuous exposure to high engine heat cycles.
Worn guide flats create excessive clearance that allows lifters to rotate off-axis within the lifter bore. If a lifter turns even slightly out of parallel with the cam lobe, it skids rather than rolls, destroying roller wheels instantly upon engine turnover.
Measuring Pushrod Length and Setting Target Preload
Operating lifter preload must be verified using an adjustable pushrod length checker with the lifter resting squarely on the camshaft base circle. Never assume factory-length pushrods will maintain correct plunger depth when installing aftermarket lifters.
Aim for an operating preload between 0.025 to 0.060 inches based on specific lifter manufacturer specifications. Standard-travel hydraulic plungers typically require 0.040 to 0.060 inches of preload, whereas short-travel lifters operate within a tighter 0.025 to 0.035-inch window to prevent valve float at high RPM.
Account for all machining alterations when calculating final pushrod length. For example, milling cylinder heads 0.030 inches lowers the rocker shaft closer to the base circle, effectively increasing lifter preload by roughly that same 0.030-inch dimension.
Leaving stock pushrods in place after a 0.030-inch mill can over-compress the plunger and hang the valves open. Calculate the net difference using your length checker, then install stiff 0.080-wall pushrods ordered to the exact corrected length to resist valvetrain deflection.
Key Takeaways
-
✓
Engineering details: Upgraded lifter bodies feature precision-ground hydraulic plungers and hardened roller bearings to resist low-RPM idle oil starvation. -
✓
MDS compatibility: Non-MDS lifters feature solid bodies, whereas MDS lifters utilize locking pins and internal springs actuated by solenoid oil pressure. -
✓
Root-cause facts: Premature roller pin deflection and needle bearing wear flat-spot the lifter, ultimately grinding down the camshaft lobe. -
✓
Ticking diagnosis: Lifter chirping or mechanical tapping follows engine RPM directly, distinguishing failed roller bearings from standard warped exhaust manifold leaks. -
✓
Assembly specs: Proper yoke alignment and setting pushrod preload between 0.040 and 0.075 inches are mandatory to prevent valvetrain noise.
❓ Frequently Asked Questions
1
What are Q construction lifters on a Hemi?
Q construction lifters on a Hemi are heavy-duty hydraulic roller lifters designed with precision internal metering and strengthened needle bearings. They deliver reliable oiling information to pushrods while tolerating high valve spring pressures, significantly reducing the probability of roller seizure and camshaft lobe wiping across modern Gen III Chrysler Hemi engines.
2
How do MDS and non-MDS Hemi lifters differ?
MDS lifters feature internal deactivation pins controlled by computer-actuated oil solenoids to collapse the lifter and shut down cylinders under light loads. In contrast, non-MDS units utilize a continuous, rigid hydraulic plunger design, delivering greater high-RPM valvetrain stability, simplified oiling details, and enhanced durability for performance builds.
3
Why do factory Gen III Hemi lifters fail prematurely?
Factory Hemi lifters often fail due to prolonged engine idling, which starves the top-end valvetrain of adequate splash lubrication. Insufficient oil flow across the roller axle leads to needle bearing overheating, roller pin deflection, and mechanical binding that quickly grinds down the intake or exhaust camshaft lobes.
4
What technical insights help diagnose a failing Hemi lifter?
A failing lifter creates a sharp, metallic ticking or chirping sound that increases proportionally with engine RPM and does not quiet down after warm-up. Contrasting with exhaust manifold leaks, which often dissipate as metal expands, failed roller lifter noise resonates directly from the valvetrain beneath the valve covers.
5
How do you correctly install Hemi lifters and set preload?
Clean all lifter bores thoroughly, lubricate rollers with high-pressure assembly grease, and slide lifters squarely into brand-new guide trays. Fasten retainers to 106 in-lbs, then measure pushrod preload to confirm 0.040 to 0.075 inches of hydraulic plunger depression, preventing valvetrain slack and premature valvetrain component wear.
6
What causes lifter failure and the infamous Hemi tick?
Detail needle bearing degradation inside the roller wheel caused by poor splash lubrication at long idle periods, leading to roller seizure, metal-on-metal cam lobe grinding, and audible mechanical ticking.